Hey folks, let’s cut to the chase—if you’re in the business of moving bulk materials, a bucket elevator isn’t just a “box with buckets on a chain” (or belt, for that matter). I’ve been supplying these workhorses for over a decade now, and the single biggest factor that separates a elevator that runs 24/7 without a hiccup from one that’s breaking down every other week? Material properties. Most folks fixate on the motor size or bucket shape, but skip the stuff that actually makes the whole thing work. Let’s break this down like we’re talking shop at a trade show, no stuffy jargon—just real, on-the-job truths. Bucket Elevator
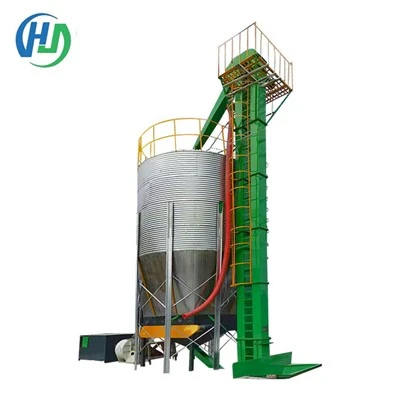
First off, let’s define what we’re actually talking about here: material properties, not just “is it heavy” or “is it dusty.” We’re digging into things like abrasiveness, moisture content, cohesiveness, and density. Each of these hits your elevator different, and picking the wrong setup to match? You’re looking at downtime, part replacements, and even safety hazards that could’ve been avoided. I’ve seen it all—from a client who installed a standard elevator for abrasive alumina powder and burned through buckets in 6 months, to another whose wet wood chips were clumping so bad the buckets weren’t discharging properly. Both came to us frustrated, because their original supplier didn’t even ask the basics about the material they were handling.
Let’s start with abrasiveness, because that’s the #1 killer of elevator components. Abrasive materials—think gravel, sand, ores, cement clinker—are like sandpaper rubbing against your buckets, chains, and liners. If you use a standard mild steel bucket for these, you’re basically asking for metal loss. Mild steel is cheap, yeah, but it wears thin fast. A better move here is high-chromium steel or abrasion-resistant (AR) steel—we stock both, but AR steel’s a go-to for most folks moving abrasive bulk because it doesn’t crack when it takes a hit, unlike some harder alloys. Wait, and it’s not just the buckets— the chain links get beat up too. For abrasive materials, we recommend double-pitch roller chains instead of standard leaf chains? No, wait, leaf chains actually hold up better under constant abrasion for vertical lifts, right? Wait, let me correct that—leaf chains have more surface area contacting the sprockets, so they wear slower than roller chains in abrasive environments. I messed that up once with a construction materials client, and we swapped out leaf chains, cut their chain wear by 40% in the first 3 months. That’s a real win.
Next up: moisture content. This one’s tricky because moisture can turn even easy-to-handle materials into a nightmare. If you’re moving something wet—like agricultural grains, distillers’ grains, or even municipal sludge—too much moisture makes materials sticky. Sticky material doesn’t discharge from the buckets when they tip over at the head pulley. Instead, it sloughs off mid-vertical lift, creates buildup on the casing, and weighs down the chain, leading to stretched links or even a broken drive shaft. I had a feed mill client a couple years back whose corn had 18% moisture content—way higher than the 12% we recommend for grain. Their buckets were caked so bad, they were only moving 60% of the capacity the elevator was rated for. We fixed it by swapping their standard smooth buckets to buckets with internal ribs to break up clumps mid-lift, and added a small vibrator at the head pulley to dislodge any leftover material. They got their full capacity back, no more clogs. On the flip side, too little moisture? Some materials get statically charged, especially fine powders like plastic pellets or flour. Static causes fine particles to stick to bucket sides and casing, leading to buildup that can throw the belt (if you’re using a belt elevator) or derail a chain. We add antistatic coatings to buckets for these jobs, and it cuts buildup by 70%—simple fix, big difference.
Cohesiveness is related to moisture but a separate beast. Cohesive materials are the ones that stick to each other more than they stick to metal—think clay, wet sugar, or fine fly ash. For these, you can’t just use a standard “centrifugal discharge” elevator—those work best for free-flowing materials that fly out when the bucket tips. Cohesive stuff needs “continuous discharge” elevators, where buckets open into each other as they go over the head pulley, so the material can spill out slowly instead of being forced. I learned this the hard way with a clay processing plant. They tried a centrifugal elevator, and the clay would ball up inside the buckets, so they were dumping 20% less material than their design spec. Switched to a continuous discharge setup with shallower buckets, and boom—their throughput jumped, and they stopped having to clean caked clay out of the casing every week. Also, for super cohesive materials, we sometimes add polypropylene buckets instead of steel. Why? Poly’s smooth surface doesn’t stick as well, and it’s lighter, so less load on the drive motor. Win-win.
Bulk density—let’s not sleep on this one. Density is how much a cubic foot of your material weighs, right? If you design an elevator for a low-density material (like expanded polystyrene, which is super light) and then use it for high-density (like iron ore pellets, which are heavy), you’re going to overload the motor, stretch chains, and even buckle the casing. I had a client who moved EPS foam and then decided to add plastic resin pellets, which are twice as dense. Their original elevator’s motor was rated for 5 HP, but they needed 12 HP to handle the extra weight. We swapped the motor, upgraded the chain to a heavier gauge, and reinforced the casing—cost them a bit, but they didn’t have to replace the entire elevator. The mistake most people make is thinking a “bucket elevator is a bucket elevator” regardless of load, but density directly impacts every moving part’s stress.
Wait, let’s touch on fine vs. coarse materials too, because that ties into wear and discharge. Fine powders—like cement, flour, or talc—can sneak into chain pins or belt splices, causing premature wear. For these, we recommend sealed chain links to keep fines out, or using a belt elevator with a cover to prevent powder from getting into the belt’s core. Coarse materials—like whole grain, gravel, or wood chips—are harder on bucket edges and sprockets. You need thicker bucket lips for coarse stuff, otherwise the edges chip off when the buckets hit the material in the boot (the bottom of the elevator where material is loaded). I’ve seen buckets with 1/4 inch lips crack when moving 2-inch wood chips, but 1/2 inch AR steel lips? No problem.
Now, let’s talk about real-world, on-the-job impacts so you know this isn’t just theory. Last year, a mining client came to us complaining their bucket elevator was down 3 days out of every 5. They were moving copper ore, which is super abrasive. They had a standard steel elevator with leaf chains. We tested their buckets—1/8 inch mild steel, worn through in 4 months. Their chain links were pitted so bad, they had to replace links every 2 months. We swapped them to high-chromium buckets (3/8 inch thick) and heavy-duty leaf chains, plus added replaceable liners to the casing where material is loaded. Now, their buckets last 18 months, chains last 12 months, and downtime dropped to 1 day a month. That’s not just better performance—that’s thousands in saved labor and replacement costs.
Another example: a flour mill that had constant dust explosions (yeah, that’s a real hazard with fine, dry powders). Their original elevator used steel buckets, which generate static when fine flour rubs against them. We switched to antistatic polypropylene buckets, bonded the casing’s joints to ground, and added a spark arrestor at the head pulley. No more sparks, no more explosion risks, and they cut buildup by half. Safety’s a big one here—ignoring material properties isn’t just bad for productivity, it’s dangerous.
Now, let’s get to the stuff you can do right now, before you even order an elevator. First, don’t just tell your supplier “I need a bucket elevator for my material”—tell them exactly what that material is. If it’s a powder, give a mesh size (how fine it is). If it’s wet, tell them the moisture percentage (you can test this with a cheap moisture meter, no lab needed). If it’s abrasive, ask “what’s the hardness of this material?” (Mohs scale, easy to look up). Second, match the discharge type to your material. Free-flowing grains? Centrifugal is fine. Wet clay? Continuous is non-negotiable. Third, don’t skimp on the components for tough materials. AR steel buckets cost a bit more up front, but they last 3x longer than mild steel. Sealed chains add a small cost but cut wear by 50%.
I get it—you don’t want to overspend on an elevator, but buying cheap and replacing parts every couple months ends up costing way more. At the end of the day, a bucket elevator’s performance lives or dies on how well it’s matched to the material it’s moving. I’ve been doing this long enough to tell you: most elevator headaches are preventable, you just have to pay attention to the material, not just the price tag.
If you’re in the market for a new bucket elevator, or your current one is acting up and you can’t figure out why—hit us up. We don’t just sell parts or elevators; we’ll sit down with you, ask you all the right questions about your material, and help you build something that runs as long as you need it to. No guesswork, no jargon, just solutions that actually work for your operation.
Grain Cleaning Fan References
- Bulk Material Handling: Design, Operation, and Maintenance, 3rd Edition, E.D. Stobbs, Elsevier, 2010
- ASME B20.1 Safety Standard for Conveyors and Related Equipment, American Society of Mechanical Engineers, 2018
- Wear of Materials in Bulk Handling Equipment, K.C. Mills, Journal of Materials Processing Technology, Vol. 106, No. 1-3, 2000
- Agricultural Bulk Materials: Properties and Handling, R. Zhang, St. Joseph Press, 2015
Henan Huinong Machinery Co., Ltd.
Henan Huinong Machinery Co., Ltd. is one of the most professional bucket elevator manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to buy discount bucket elevator from our factory. We also accept customized orders.
Address: No. 6, Northeast Corner of the Intersection of Renmin Road and Zhujiang Road, New District, Huaxian County, Henan Province
E-mail: frank.tang@huinongmachinery.com
WebSite: https://www.huinongmachinery.com/
