If you’ve ever held a smartphone, a power drill, a medical pacemaker, or even the tiny circuit board in a smart watch, you’ve held an electronic stamping part. As someone who’s spent the last 12 years running a small, specialty electronic stamping parts supplier—one that’s worked with automotive, aerospace, and medical device brands to turn raw metal into precision components—I get asked this question all the time by new clients and curious hobbyists alike: What actually goes into making these parts? It’s not just shoving a sheet of metal into a press and calling it a day. Every tiny pin, terminal, and contact that powers your devices is the result of a precise, multi-step process that balances speed, accuracy, and material integrity. Today, I’m pulling back the curtain on our shop floor to walk you through exactly how electronic stamping parts are made, straight from the perspective of a supplier who’s messed up enough runs to know every pitfall to avoid. Electronic Stamping Parts
First, let’s start with the part that makes or breaks every finished component: the material. Electronic stamping relies on metal foils and sheets that are thin, conductive, and corrosion-resistant—think copper, brass, beryllium copper, or stainless steel, but not the thick steel you’d use for a car door. At our shop, we source materials certified for electrical performance, not just structural strength. For a terminal that connects a car battery to its alternator, we use pure copper because it has the highest electrical conductivity of any common metal. For a tiny spring contact inside a hearing aid, we opt for beryllium copper, which bends thousands of times without breaking and resists tarnishing that would mess with signal flow. The material comes to us in large coils—sometimes 5,000-pound rolls that are nearly 3 feet wide, sometimes smaller rolls for prototype runs. We never skip a pre-production material check: we test for thickness consistency (even a 0.001-inch variation can throw off a stamping run) and surface purity (a single fingerprint or microscopic rust spot can ruin a contact’s ability to conduct electricity). Last year, we had a client’s prototype for a medical device come back defective because the material they’d sourced had hidden inclusions; since we test every coil, we caught it before we touched a single die, saving the client three months of delays. That’s the kind of attention to detail our team lives for.
Next, the blueprint. Before we even touch a sheet of metal, our engineering team works hand-in-hand with the client’s design team to translate their idea into a manufacturable part. This is where we earn our keep, especially when clients come to us with a sketch or a 3D model and no idea how to make it affordable. For example, a startup that makes wireless earbuds once brought us a tiny metal clip to hold the charging case closed; their initial design called for 12 individual parts, which would have been slow and expensive to assemble. Our engineers suggested a single stamped part that integrated all the clip’s functions, cutting production costs by 40%. During this step, we also work out the stamping method: for high-volume runs (like 1 million terminals a year for a smartphone), we use progressive stamping, which uses a series of dies to shape the part step-by-step as the metal coil feeds through the press. For low-volume prototypes or custom parts, we use blanking and fine blanking, which cuts individual parts one at a time with ultra-sharp dies for tight tolerances. We also run finite element analysis (FEA) to simulate how the metal will behave under the press, making sure it won’t crack or warp during shaping. This step is where most avoidable mistakes happen; cutting corners here leads to parts that break or don’t fit when the client goes to assemble their product.
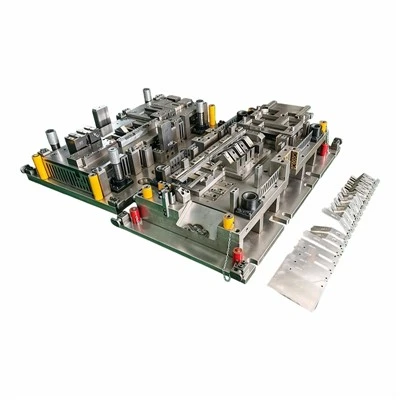
Once the design is locked in, it’s die time. Dies are the custom-made steel tools that actually shape the metal, and they’re the most critical piece of equipment in our shop. Think of a die like a cookie cutter, but made from hardened tool steel that can withstand millions of presses without dulling. For progressive stamping dies, we build a series of stations: the first station punches pilot holes to align the metal coil perfectly, the second cuts the outline of the part, the third bends tiny tabs, the fourth cuts notches for connection points, and so on, until the finished part pops out at the end of the line. Building a die takes 4 to 6 weeks, depending on the complexity. Last year, we built a die for a aerospace terminal that had 17 individual stations and tolerances of ±0.0005 inches— that’s thinner than a human hair. The machinists who build our dies are some of the best in the industry; they’ve been doing this for 20+ years, and they take pride in making a tool that will produce thousands of perfect parts without a single misfeed. We also test each new die with a sample run of 100 parts before we put it into full production, checking for burrs (sharp edges that can short circuit electronic parts), misalignments, or uneven bends. If even one part is off by 0.0001 inches, we send the die back for tweaks—no exceptions. A bad die doesn’t just ruin parts; it wastes hundreds of pounds of metal and thousands of dollars in time.
With the die tested and approved, we move to the stamping press itself. These aren’t the big, noisy presses you see in car factories; our stamping presses range from 5-ton machines for tiny medical parts to 200-ton machines for larger automotive terminals. The press feeds the metal coil through the die at a steady, consistent speed—some high-volume presses can run 1,200 strokes per hour, which means a new part every 3 seconds. Speed is great for throughput, but consistency is everything. Our presses are loaded with sensors that track force, alignment, and part thickness every single stroke. If the press detects a variation in the force needed to punch or bend the metal, it automatically stops to check for a problem—no more ruining a whole batch of parts because of a tiny misfeed. During a typical run, our operators do a first-part check every 1,000 parts, measuring dimensions with calipers and coordinate measuring machines (CMMs) that can read parts with microscopic accuracy. They also do visual checks for burrs or surface defects, since even a tiny scratch on a contact point can cause a device to fail later on. A few months ago, we had a client run a 100,000-part batch of terminals that were perfect on the first check, but we caught a slight burr on 27 parts on the 50,000th part check. It turned out the die had a tiny chip from a piece of metal that got caught, and we fixed it mid-run, saving our client from having to scrap the whole batch when they got their parts. That’s the kind of proactive quality control that separates good suppliers from great ones.
But stamping doesn’t end when the part comes out of the press. The parts have to go through secondary operations that make them functional for electronics. The first of these is deburring: even with sharp dies, stamping leaves tiny, sharp burrs along the edges of the parts. For small parts, we use a vibratory tumbler, where we load the parts into a tub with ceramic beads and a mild polishing compound that bounces the parts around, sanding down burrs without damaging the delicate contact points. For larger parts, we use a chemical deburring process that dissolves sharp edges without altering the part’s shape. Next is surface finishing, which is critical for electrical performance and corrosion resistance. Most electronic stamping parts need a plating or coating: gold plating for contacts that need ultra-low resistance in high-end electronics, tin plating for automotive parts that need to resist rust, nickel plating for parts that go inside harsh environments like aerospace engines. Plating is a precise process; too thick, and the part won’t fit into its housing; too thin, and the plating will wear off within a year of use. We work with certified plating partners that meet industry standards (like ISO 9001 and IPC-A-610, the global standard for electronic assembly quality) to make sure the finish is consistent and meets the client’s specifications. We also do adhesion tests for plating, scratching the surface with a tool to make sure the coating doesn’t peel off, and salt spray tests to make sure it won’t corrode in humid or harsh conditions. For parts that need to be soldered directly onto circuit boards, we also do a flux treatment to make sure the solder sticks properly, another step that’s easy to skip but leads to major failures down the line.

Once the secondary operations are done, the parts go through final inspection and packaging. This is the last line of defense before parts leave our shop. We do a 100% visual inspection for every custom or high-value part, checking for any surface defects, plating inconsistencies, or dimensional errors. For high-volume runs, we use automated vision systems that scan each part in milliseconds, catching defects that a human eye might miss. We also run functional tests: for a terminal, we test the pull force to make sure it fits securely into its connector; for a contact spring, we test its spring rate to make sure it presses hard enough to make good electrical contact without breaking. The final step is packaging, and this is where we’ve had to learn some hard lessons. Years ago, we shipped parts in generic plastic bags, and when our client opened them, the parts had shifted and scratched each other, ruining a whole shipment. Now, we package parts in anti-static packaging (critical for electronic parts that can be damaged by static electricity) with custom foam trays that hold each part in place, so they don’t move during shipping. We also include a batch certificate for every shipment, listing the material, die number, plating thickness, and inspection results, so our clients can track every part back to its source.
Metal Stamping Dies At the end of the day, electronic stamping parts are more than just tiny metal components. They’re the unsung heroes of every device we use, and making them well takes a mix of old-school craftsmanship and modern technology. I’ve spent thousands of hours on our shop floor, watching our team adjust dies, troubleshoot press issues, and check parts late into the night, and I can tell you there’s no shortcut to doing this right. If you’re a designer, engineer, or procurement specialist looking for a reliable partner for your electronic stamping parts, we bring that 12 years of hands-on experience, attention to detail, and commitment to quality to every job. We work with clients from prototype runs of 100 parts to high-volume runs of millions, and we’re ready to help you turn your design into a perfect, functional component for your product. To discuss your project, feel free to reach out at your convenience.
References
- IPC Association Connecting Electronics Industries. IPC-A-610: Acceptability of Electronic Assemblies. IPC, 2022.
- Groover, M.P. Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. 7th ed., Wiley, 2020.
- European Stamping Association. Best Practices in Precision Metal Stamping for Electronics. ESA, 2021.
- ASTM International. Standard Test Methods for Mechanical Testing of Stamped Metal Parts. ASTM B117, 2019.
Dongguan Changdong Tool & Die Co., Ltd.
With abundant experience, we are one of the most reliable electronic stamping parts manufacturers and suppliers in China. Please feel free to buy advanced electronic stamping parts made in China here from our factory. Good service and quality products are available.
Address: No. 56-B, Fumin South Road, Dalang Town, Dongguan City, Guangdong Province, China
E-mail: sales@stamping-die.com
WebSite: https://www.metalstampingdie.com/
