Hey there, if you’re reading this, chances are you’ve got a cutting wheel that’s been misbehaving—you’re chipping edges, getting weird sparks, or it’s wobbling so bad it feels like it’s gonna fly off the tool. I’m gonna cut to the chase here (pun intended), I’ve been supplying cutting wheels for over a decade, and let me tell you, 90% of the headaches customers face aren’t from a bad wheel—they’re from a wheel that’s not aligned right. I see it every single week: guys rush the alignment, skip a step, and then end up blaming the product. Today, I’m breaking down exactly how to get that alignment right, no fancy tools needed, just some common sense and a little patience. Cutting Wheels
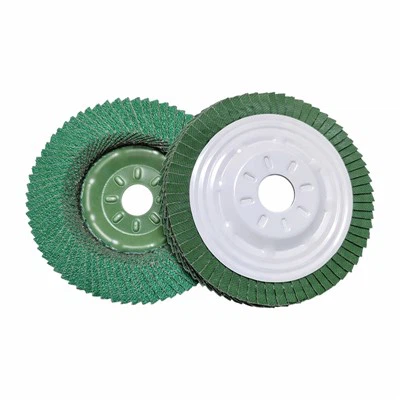
First off, let’s get one thing straight—what “aligning a cutting wheel” actually means. It’s not just shoving the wheel onto the arbor (that’s the metal shaft on your grinder, for the uninitiated) and tightening the nut. It’s making sure the wheel spins perfectly flat, no side-to-side wiggle, and that the pressure from the flanges (those round metal plates that hold the wheel tight) is even all around. If it’s off even a hair, that wheel’s gonna wear unevenly, break early, or worse, send a fragment flying. I’ve heard too many horror stories from customers who skipped this and had to take a trip to the ER—don’t be that guy.
Let’s start with prep, because you’d be surprised how many people skip this part. First, turn off the grinder and unplug it. I don’t care if you just put it down for a second—this is non-negotiable. No one wants a spinning wheel catching a finger. Next, grab your new wheel (or the one you’re trying to set up), the arbor nut wrench that came with your grinder, a clean rag, and maybe a marker. Oh, and if your grinder has any old gunk on the arbor or flanges, wipe that down first. Rust, old wheel dust, or leftover resin from a past wheel will throw everything off. I once had a customer bring back 20 wheels in a month because they wouldn’t stay aligned—turns out he was leaving old metal shavings on the flanges. Common mistake.
Now, let’s talk flanges. The two metal plates that hold the wheel—they’ve got to be clean, flat, and the right size. I’ve seen people use a flange that’s too small, so only the center of the wheel is held, which makes it flex when you cut. Rule of thumb: each flange has to cover at least 1/3 of the wheel’s total diameter. If yours are beat up, have dents, or rust spots, replace them. You can buy replacement flanges cheap, and it’s not worth risking a wheel imbalance over a $5 part. Also, most grinders have a small offset on the flanges—make sure you put them on the right side. The concave side should face the wheel, not flat against it. That’s another rookie move I see all the time.
Next, mounting the wheel. Slide it onto the arbor, make sure it’s sitting dead center between the two flanges. Don’t force it—if it’s sticking, double-check for gunk. Now, here’s the part most people mess up: tightening the nut. You don’t need to crank it like you’re trying to move a boulder. Too much pressure will warp the wheel, make it crack, or throw off the alignment. Too little, and it’ll spin. What’s the sweet spot? For most 4.5-inch cutting wheels (the most common size we supply), tighten the nut with your wrench until it’s snug—then give it about a quarter turn more. If you’ve got a grinder with a lock button to hold the arbor in place, use it. Don’t hold the arbor with your hand while tightening—you’ll slip and over-tighten, I promise.
Okay, so you’ve got the wheel on, nut tightened. Now the real test: checking for alignment. Most people skip this and go straight to cutting, which is why they have problems. Here’s how to do it right. First, put on your safety glasses (duh, but I have to say it—half the accidents happen because people skip PPE). Then, turn the grinder on and let it spin for 10 seconds. Stand to the side, not in front of it (if something breaks, that’s the safest spot). Watch the wheel. If it’s wobbling side to side, that’s bad. If it’s spinning in a perfect flat circle, you’re golden.
Wait, but what if it’s wobbling? Don’t panic. Sometimes it’s the wheel itself, but most of the time it’s the installation. Let’s troubleshoot. First, turn off the grinder and unplug it again. Loosen the nut, pull the wheel off, and flip it around. Sometimes a tiny defect in the wheel’s center hole or a little dust on one side is throwing it off. If flipping it works, great. If not, double-check the flanges again. Are they on straight? Any dents? If they look good, try a different wheel. Sometimes a cheap wheel has a slightly off-center core, and even if you align it right, it’ll wobble. That’s why I always tell customers to stick with quality wheels—we test every single one for core alignment before they leave our warehouse, so you don’t have to guess.
Another trick we use at the shop: the marker test. Once you’ve got the wheel on and the nut loose (before tightening all the way), take a dry-erase marker and draw a straight line across the face of the wheel, all the way around. Then, spin the wheel by hand, and watch the line. If the line stays perfectly straight the whole time, it’s aligned. If it wiggles or curves, you’ve got a problem. This works way better than just staring at it spinning, especially for new guys.
Wait, what if you’re changing wheels on a regular basis? Like, if you’re a fabricator or a maintenance tech who goes through 10 wheels a day. The alignment process stays the same, but there’s a quick check you can do between changes. After you tighten the nut, before you turn it on, give the wheel a light spin by hand with your finger. If it spins smooth, no wobble, you’re good. If it catches or feels like it’s dragging, take it apart and check again. That saves you from firing up the grinder just to find out it’s misaligned.
I also want to talk about common mistakes that mess up alignment over time. First, using a wheel that’s the wrong size for your grinder. If your grinder takes a 4.5-inch wheel, don’t force a 5-inch one on there—you’ll have to adjust the flanges, and that throws everything off. Second, not replacing flanges when they’re worn. Flanges get dented from dropping the grinder, rust from being in a dusty shop, and after a while, they don’t sit flat anymore. We recommend replacing flanges every 6 months if you use your grinder a lot, or whenever you see a dent. Third, tightening the nut in a circle, not just one spot. Wait, no—when you tighten the nut, you should do it evenly. If you tighten one side all the way first, you’ll warp the wheel. Tighten it a little, then spin the arbor, then tighten a little more, alternating until it’s snug. That distributes the pressure evenly across the wheel, which keeps it aligned.
Oh, and let’s not forget about wheel conditioning. When you get a new wheel, it’s got a protective coating or a layer of resin on the surface. If you just start cutting right away, that coating can make the wheel bind or wear unevenly, which will throw off the alignment. The fix? Run it on a piece of scrap metal for 10 seconds before you use it for real. That breaks in the wheel, removes the excess coating, and makes sure it spins true. I can’t tell you how many customers skip that step and then think their wheel is misaligned—it’s just the surface coating.
Wait, what if you’re using a cut-off saw (the big stationary ones, not handheld grinders)? A lot of the same rules apply, but there’s a couple extra steps. First, make sure the vise on the saw is tight, because if the workpiece moves, it can pull the wheel off alignment. Second, check the blade guard (or wheel guard) is adjusted correctly—if it’s covering too much, it can rub the wheel, throwing it off. Third, for larger wheels (like 12-inch ones), make sure the arbor has a proper lock washer. Those work better than just a nut alone for bigger wheels, because they distribute the pressure more evenly. I’ve seen a 12-inch cut-off wheel fly off a saw once because the guy skipped the lock washer—scary stuff.
Now, let’s get to the troubleshooting part, because even if you do everything right, sometimes you still get a wobble. First, check the arbor itself. Is it bent? If you’ve dropped your grinder or hit it really hard, the metal shaft might be bent, which will make the wheel wobble no matter what. You can check this by spinning the grinder with no wheel on it—if the arbor spins straight, it’s fine. If it’s bent, you’ll have to replace the arbor, which is a cheap part. Second, check the wheel for damage. If it’s got a crack, chip, or is warped, it’ll never align right. Always inspect your wheel before mounting it—no matter how good the brand is, a bad wheel is a bad wheel. Third, make sure you’re using the right wheel for the material. If you’re cutting stainless steel with a general-purpose wheel, it’s gonna wear unevenly, which will make it wobble as it gets thinner. We sell specific wheels for different materials—steel, stainless, aluminum, even stone—so make sure you’re matching the wheel to the job.
Here’s a pro tip I learned from my dad, who started selling cutting wheels back in the 80s: after you align the wheel, give it a gentle press against a piece of flat scrap metal while it’s spinning. If it cuts evenly all around, no deep grooves or light spots, it’s aligned. If it only cuts on one side, that means the wheel is tilting, and you need to loosen the nut, adjust the wheel, and tighten again. That’s a quick way to test it without having to stare at it spinning.
Alright, let’s wrap this up with a quick recap, because I know you guys are busy and don’t want to read a novel. Step 1: Unplug the grinder, clean arbor and flanges. Step 2: Make sure flanges are flat, the right size, and on correctly (concave side to wheel). Step 3: Mount wheel dead center, tighten nut a quarter turn beyond snug—don’t overdo it. Step 4: Spin the grinder, check for wobble. Step 5: If wobble, flip wheel, check flanges, or try a new wheel. Step 6: Condition the wheel on scrap metal for 10 seconds before using. Step 7: Check for arbor bend or wheel damage if wobble persists.
Now, if you’re still having trouble, or you need help picking the right cutting wheel for your grinder and material, hit me up. We supply all types of cutting wheels for handheld grinders, cut-off saws, everything from 3-inch to 16-inch. We test every product to make sure they align true right out of the box, so you don’t have to waste time troubleshooting. Just reach out to our team, tell me what you’re working with, and we’ll get you set up. No jargon, no hidden fees, just good wheels and honest advice.
Don’t cut corners on alignment—it’s the difference between a safe, smooth job and a trip to the hospital. I’ve seen it too many times. Do it right, and your wheels will last longer, cut straighter, and save you money in the long run. Alright, go get that alignment done, and if you need supplies, I’m here.
Aluminum Oxide Flap Disc References
- Abrasive Safety Handbook. Industrial Abrasive Manufacturers Association, 2021.
- "Proper Mounting and Alignment of Abrasive Cutting Wheels." Tooling Tech Journal, vol. 17, no. 3, 2022, pp. 45-52.
- Field Guide to Abrasive Wheel Maintenance. Construction Equipment Association, 2020.
Henan Yandisc Hardware Tools Co., Ltd.
Address: Zinan Road, High-tech Industrial Development Zone, Zhengzhou, Henan, China
E-mail: info@yandisc.com
WebSite: https://www.yandisc.com/
